
Detectable Equipment
Protect your brand, avoid product contamination and ensure audit compliance.
Designed for the food industry. Stocked for next day delivery.*


Home of the Retreeva Global brand of detectable equipment.
UK manufactured for unrivalled quality, longevity and safety.
Tried, tested & proven for leading durability and detectability.
“Reliable company, fast delivery, quality equipment, great communication and frequent updates. The best supplier out of all that I have the pleasure of dealing with!”
QA Manager, Natures Way Foods Group

Latest Blog Posts
WEBINAR: Allergen Management: Getting the Clean Right
Part Two of our Allergen Management Series, hosted in partnership with Campden BRI, offers a closer look at completing a successful clean.
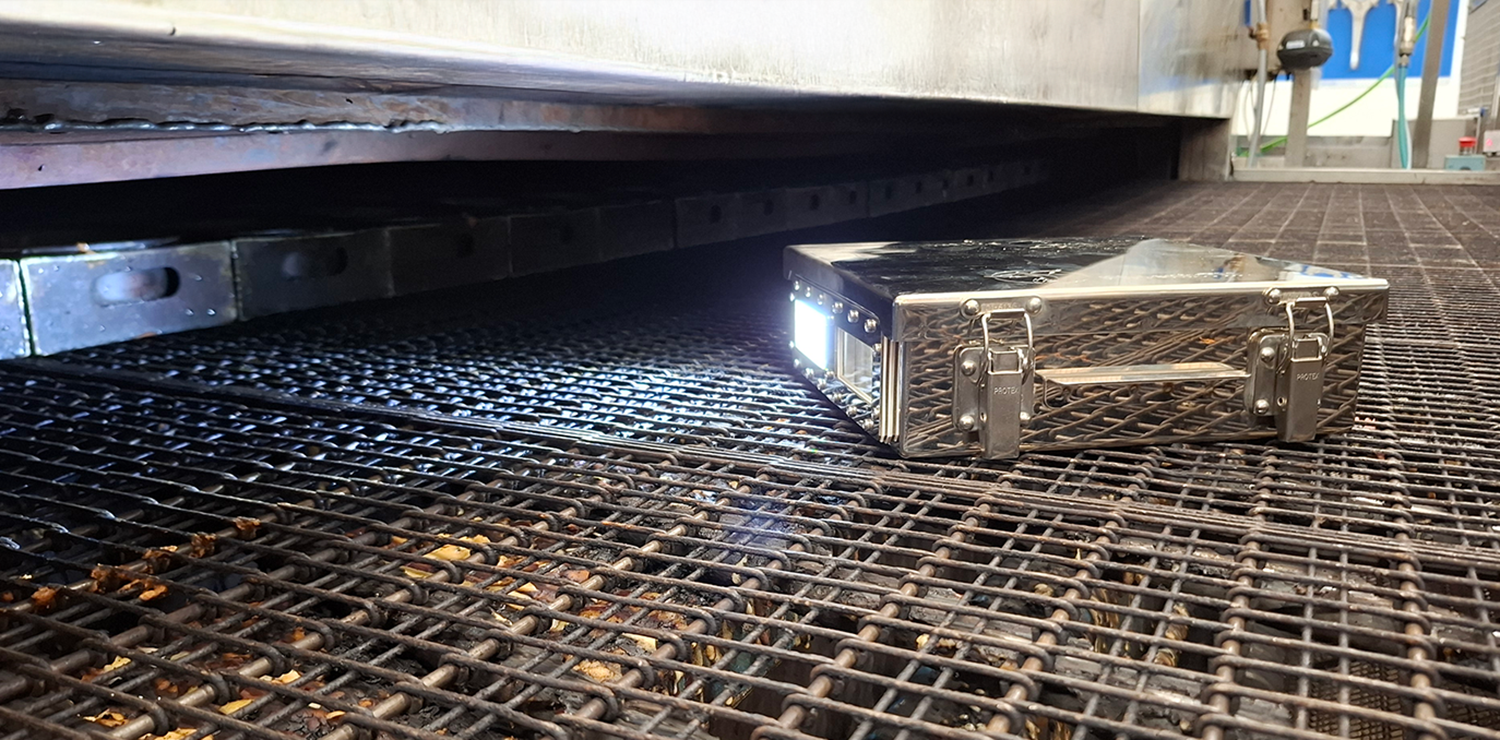
6 Benefits of In-Process Optical Monitoring in Food Manufacturing
6 benefits of In-Process Optical Monitoring in food manufacturing, from preventing cross-contamination to supporting audit preparation.

Webinar Round Up: Allergen Management: Closing the Gap
Insights from our Industry Webinar on Strengthening Allergen Management in Food Manufacturing. The first in a three-part series.
6 Benefits of In-Process Optical Monitoring in Food Manufacturing
6 benefits of In-Process Optical Monitoring in food manufacturing, from preventing cross-contamination to supporting audit preparation.


 Shadow Boards & Equipment Storage
 Visual Management
 Hygiene & Production Equipment
 Food Handling & Storage Containers
 Instrumentation and Monitoring
 Calibration & Service
 Segregation & Washdown Covers
 Detectable Equipment
 Specialist PPE
 Stainless Steel Equipment
 Hygiene Squeegees
 Vacuum Cleaners
 Food Manufacturing
 Food Storage, Distribution & Retail
 Auditors & Food Safety Inspectors
 Food Service & Hospitality